important Takeaways
ePTFE membranes serve as essential components in various industries due to their impressive characteristics. Their ability to resist chemical attacks and maintain integrity in extreme temperatures makes them indispensable in sectors such as aerospace, automotive, and medical devices. The high permeability of ePTFE membranes enhances moisture management by allowing water vapor to escape while preventing liquid ingress. This feature is important for products that require breathability, contributing to user comfort and product longevity. Furthermore, their role in sound transmission within acoustic devices exemplifies their versatility; they facilitate clear audio by allowing sound waves to pass through while managing pressure effectively. As technology advances, ePTFE membranes are expected to see increased integration into novel applications, including smart technologies that monitor environmental conditions. Overall, the growing demand for durable and reliable materials highlights the vital role of ePTFE membranes across diverse fields.
Applications of ePTFE Membranes in Industry
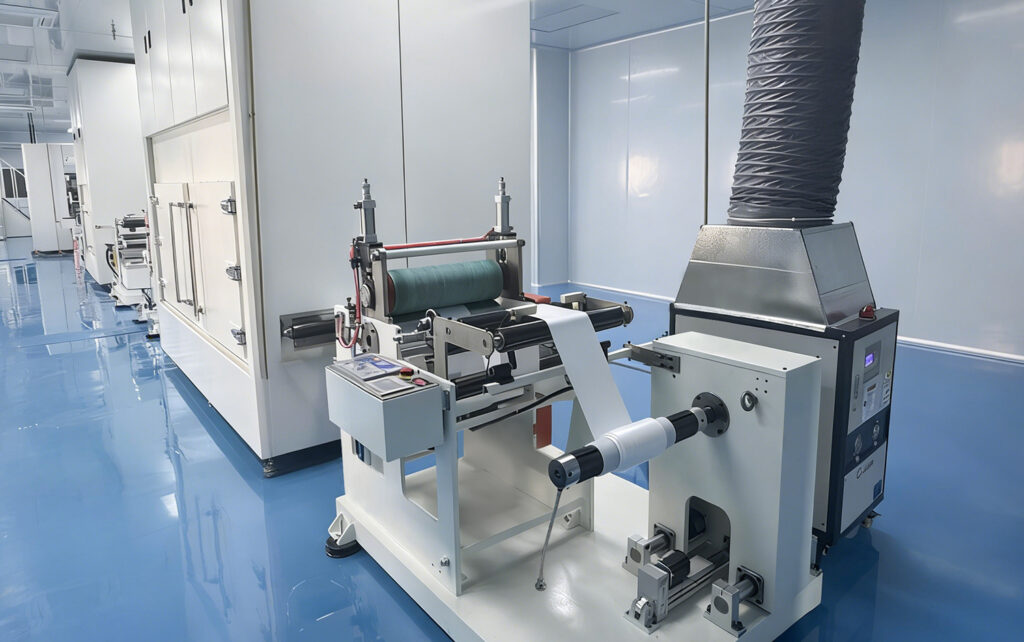
ePTFE membranes have found extensive applications across various industries due to their unique properties. Their chemical stability enables them to perform effectively in challenging environments, including high temperatures and corrosive settings. These membranes are particularly useful in the automotive and aerospace sectors, where they are used for sealing and insulating components. furthermore, ePTFE is instrumental in the medical field, serving as a barrier in filtration systems and wound dressings. It plays a role in enhancing the reliability of systems that require high-speed transmission line PTFE wrapping tape or PTFE wrapping film, ensuring efficient performance while minimizing signal loss.
In communication technologies, products like PTFE cable wrapping tape are important for maintaining signal integrity and reducing electromagnetic interference. ePTFE membranes also contribute to the manufacturing of DAC high-speed cable wrapping film, AEC high-speed cable wrapping film, and other specialized films that meet the demands of data-heavy applications. Their versatile use illustrates not only their practicality but also their importance in advancing technology across various sectors.
Chemical stability of ePTFE Membranes
The chemical stability of ePTFE membranes is one of their most notable characteristics, making them ideal for various industrial applications. These membranes resist most chemicals, including acids, bases, and organic solvents, which allows them to maintain performance integrity in harsh environments. Their inert nature means that they do not react with substances they come into contact with, ensuring that they prevent contamination and degradation over time. This stability is particularly important in the pharmaceutical and food processing industries, where product purity is paramount. also, ePTFE membranes can withstand extreme temperatures without losing their structural integrity. This resilience contributes to their longevity in demanding conditions and reduces the frequency of replacements. Consequently, manufacturers benefit from reduced operational costs and increased efficiency due to the enhanced reliability of these membranes in critical applications. Overall, the exceptional chemical stability of ePTFE membranes plays a significant role in promoting their widespread use across multiple sectors.
High permeability benefits of ePTFE
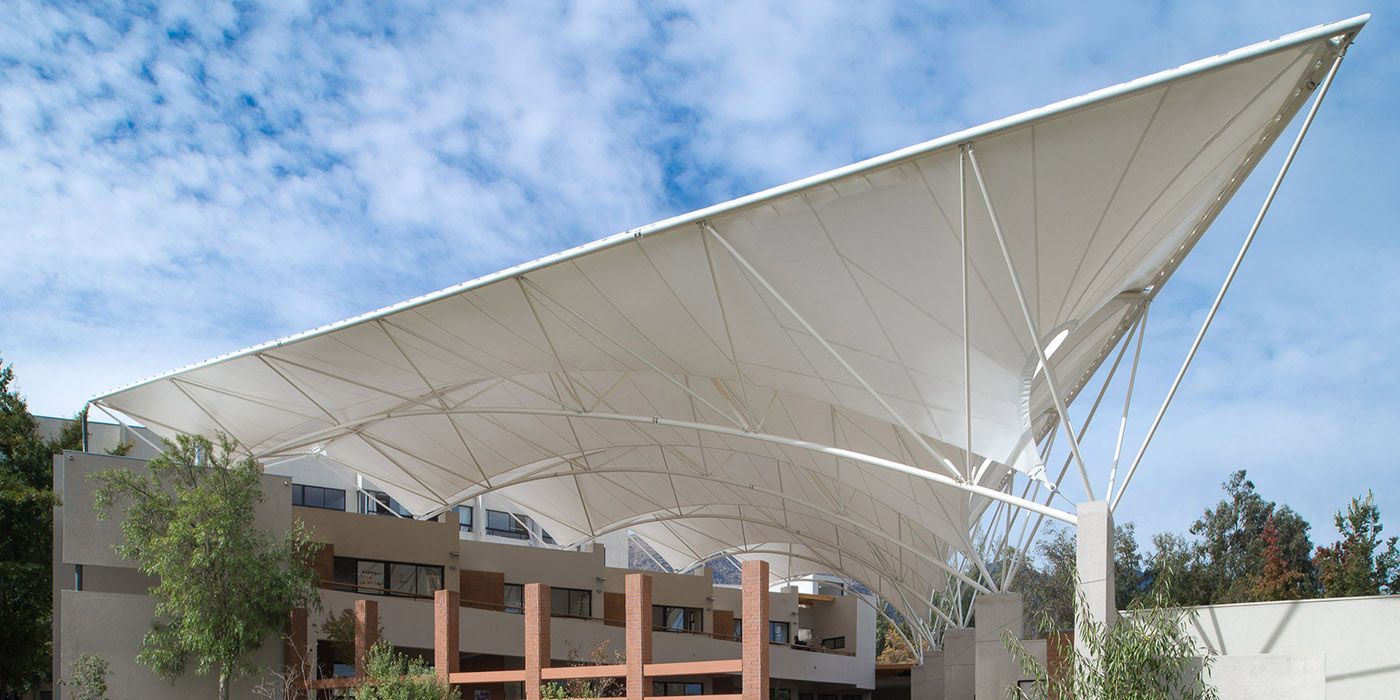
ePTFE membranes exhibit remarkable permeability, which allows them to efficiently facilitate the transport of water vapor while preventing liquid water from passing through. This unique characteristic is essential in applications where moisture management is critical, such as in clothing, outdoor gear, and building materials. The ability to maintain breathability without water ingress contributes to improved comfort and durability in various products. furthermore, the high permeability of ePTFE can help regulate internal environments by equalizing pressure differences between the inside and outside of enclosures. This property is particularly beneficial for acoustic applications, as it enables sound transmission without significant loss while managing pressure fluctuations. Furthermore, the microporous structure maintains performance stability even in extreme conditions, making ePTFE a preferred choice for industries that demand reliability and efficiency. As manufacturers continue to innovate with ePTFE technology, the advantages of high permeability will likely lead to new applications that further leverage its unique properties across diverse sectors.
Enhancing product performance with ePTFE
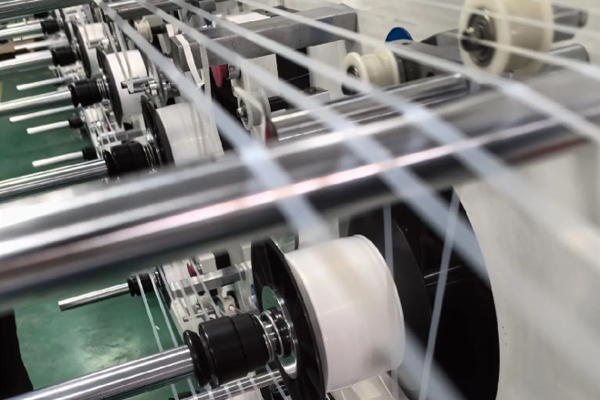
ePTFE membranes play a significant role in improving product performance across various industries. Their unique properties allow for superior moisture management while preventing contaminants from penetrating the material. This characteristic ensures that products maintain their integrity over time, which is essential in applications like medical devices and outdoor gear. Furthermore, the chemical resistance of ePTFE membranes protects products from harsh environmental conditions, thereby extending their lifespan and reliability. In industrial settings, where equipment often faces extreme temperatures or corrosive elements, ePTFE membranes contribute to enhanced performance by maintaining functionality under challenging circumstances. Manufacturers benefit from this resilience, as it leads to reduced maintenance costs and increased customer satisfaction. As industries continue to evolve and demand more reliable solutions, the enhancement of product performance through ePTFE technology remains a focal point for innovation and development.
ePTFE Membranes in Harsh Environments
ePTFE membranes are particularly well-suited for use in harsh environments due to their remarkable chemical stability and resistance to extreme temperatures and corrosive substances. These properties allow them to maintain performance when exposed to challenging conditions, enabling manufacturers to rely on them in demanding applications. Industries such as chemical processing, aerospace, and oil and gas seek materials that can withstand the rigors of their operations. ePTFE membranes provide effective barriers against moisture while allowing vapor diffusion, which is essential for maintaining material integrity in sensitive equipment. Their durability not only enhances the longevity of products but also contributes to safety by preventing leaks and failures that can arise from environmental stressors. Furthermore, these membranes often incorporate additional design features that bolster their effectiveness, ensuring they meet specific performance standards required in various applications. As industries continue to evolve, the demand for reliable materials like ePTFE membranes will likely grow, highlighting their important role in sustaining efficiency and safety within harsh operational contexts.
Role of ePTFE in Acoustic Components
ePTFE membranes play a important role in the acoustic industry by facilitating sound transmission while minimizing loss. Their unique microporous structure allows sound waves to pass through effectively, supporting the development of components such as microphones and speakers that require high fidelity. Furthermore, these membranes help maintain balanced pressure between internal and external environments, which is important for consistent sound quality. As a result, ePTFE membranes are essential for applications in hearing aids, professional audio equipment, and other consumer devices that demand optimal acoustic performance. Their chemical stability also ensures durability in various environmental conditions, contributing to the longevity of audio products. Thus, ePTFE membranes not only improve sound transmission but also improve the overall reliability of acoustic devices, making them helpful components in modern sound engineering.
ePTFE Membranes for Electronic Insulation
ePTFE membranes play an important role in electronic insulation due to their unique properties. These membranes offer excellent electrical insulation, making them suitable for high-frequency applications. Their low dielectric constant and minimal loss contribute to improved signal integrity, essential for advanced technologies like telecommunications and data transmission systems. Furthermore, ePTFE’s chemical stability ensures resistance to a wide range of harsh substances that may affect other insulating materials. This robustness enhances the longevity of electronic components while maintaining performance standards. The ability of ePTFE membranes to withstand elevated temperatures further supports their use in demanding environments, where traditional insulation materials might fail. This combination of features allows ePTFE membranes to meet the rigorous requirements of industries such as aerospace, automotive, and medical devices, where reliable insulation is important for operational success. As technology continues to evolve, the demand for such advanced insulating solutions is expected to grow, prompting further innovation in ePTFE applications within the electronic sector.
Future trends in ePTFE Technology
The future of ePTFE membrane technology appears promising as innovations emerge to address rising industrial demands. Researchers are focusing on enhancing the membranes’ functionality while retaining their chemical stability and high permeability. Development in nanotechnology is expected to lead to smaller, more efficient membrane structures, optimizing their performance for specific applications. Moreover, increased sustainability efforts are pushing manufacturers to explore eco-friendly production techniques and materials that reduce the environmental impact without compromising quality. The integration of smart technologies into ePTFE applications is gaining traction; this might include sensors embedded within membranes to monitor environmental conditions in real time. As industries continue to push for higher efficiencies and better performance, ePTFE membranes will likely play a important role in areas such as filtration systems and advanced insulation materials, further showcasing their versatility across diverse sectors.
Conclusion
the versatility of ePTFE membranes across various industries underscores their significance in modern applications. Their remarkable chemical stability and high permeability make them essential for products that must endure challenging environments. These membranes not only improve product performance but also improve the longevity of components in sectors such as aerospace, automotive, and medical devices. As industries face increasing demands for efficiency and reliability, the role of ePTFE membranes will become even more important. Innovations in ePTFE technology, driven by sustainability and advancements in materials science, promise to elevate these membranes’ capabilities further. Emerging trends indicate a shift towards smart applications that integrate monitoring systems within ePTFE structures, which could revolutionize how we approach product design and performance assessment. Overall, the ongoing development of ePTFE technology will likely yield new opportunities and applications that continue to support a wide range of industrial needs.
FAQs
What are ePTFE membranes?
ePTFE membranes are polytetrafluoroethylene materials expanded into a porous structure, notable for their chemical stability and high permeability.
What industries commonly use ePTFE membranes?
ePTFE membranes are used across various industries, including automotive, aerospace, medical, and electronic sectors, to provide reliable sealing and insulation properties.
How does the chemical stability of ePTFE membranes benefit their applications?
The chemical stability of ePTFE membranes allows them to resist harsh chemicals and extreme temperatures, making them suitable for environments where product integrity is important.
Can ePTFE membranes handle moisture effectively?
Yes, ePTFE membranes maintain breathability while preventing liquid water ingress, making them ideal for applications requiring moisture management.
What role do ePTFE membranes play in acoustic devices?
ePTFE membranes facilitate sound transmission in acoustic devices while minimizing loss, proving essential for high quality microphones and speakers.
Are there ongoing advancements in ePTFE technology?
Yes, ongoing research focuses on enhancing the functionality of ePTFE membranes through innovations like nanotechnology and sustainable production techniques.