main Takeaways
PTFE raw material tape stands out in various industrial applications due to its remarkable attributes. Its exceptional chemical resistance ensures that it can effectively withstand exposure to harsh chemicals without compromising its integrity. This property is essential in industries such as chemical processing and manufacturing, where product safety and reliability are critical. furthermore, the durability of PTFE tape under extreme temperatures further establishes its role as a dependable sealing solution. Its non-stick characteristics facilitate easy maintenance and minimize contamination risks, particularly in the food processing sector. Furthermore, PTFE tape is critical in electrical insulation applications, providing excellent dielectric properties and enhancing the safety of electrical systems. The versatility of PTFE raw material tape not only improves operational efficiency but also contributes to reduced maintenance costs across various manufacturing processes. Overall, its unique blend of properties highlights the importance of PTFE tape in meeting the diverse needs of modern industry while ensuring efficiency and safety.
Applications of PTFE Raw Material Tape in Industry
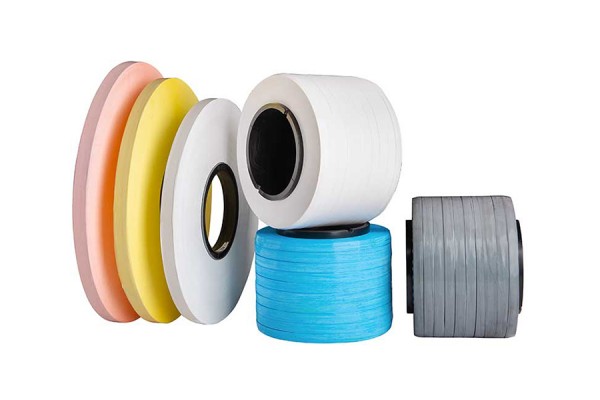
PTFE raw material tape finds extensive applications across various industries due to its unique properties. In the field of electrical insulation, PTFE Thread Seal Tape is vital for preventing leaks and ensuring the integrity of connections. This tape offers high resistance to chemicals and heat, making it suitable for sealing applications in environments exposed to aggressive substances. PTFE wrapping film is commonly used in manufacturing processes, providing surface protection and insulation for wires and cables.
High speed transmission line PTFE wrapping tape is essential in telecommunications, especially for high-speed and high-frequency cable wrapping. It ensures signal integrity while minimizing loss, which is critical for performance. Moreover, AEC high-speed cable wrapping film and DAC high-speed cable wrapping film are optimized for demanding setups where durability and reliability are paramount.
also, industries involved in food processing utilize PTFE cable roll coating to create non-stick surfaces that simplify cleaning processes. The versatility of these materials enables innovations across sectors, showcasing their importance in modern manufacturing and service operations.
Advantages of Using PTFE Tape for Sealing
PTFE tape offers significant advantages for sealing applications across various industries. Its excellent chemical resistance ensures that it can withstand exposure to a wide range of corrosive substances without degrading. This property makes PTFE tape ideal for use in chemical processing and manufacturing, where durability and reliability are paramount. also, the tape’s non-stick qualities prevent materials from adhering to its surface, allowing for easy removal and maintenance. This feature is especially beneficial in applications where regular access is necessary, as it reduces downtime and enhances operational efficiency. Furthermore, PTFE tape maintains a stable performance over a broad temperature range, making it suitable for environments that experience extreme heat or cold. Overall, these attributes make PTFE tape a important choice for ensuring effective sealing solutions in demanding conditions.
Chemical resistance of PTFE Raw Material Tape
PTFE raw material tape is well-known for its outstanding chemical resistance, making it a preferred choice in industries that handle corrosive substances. This resistance applies to a broad spectrum of chemicals, including acids, bases, and solvents. Because of its unique molecular structure, PTFE does not easily react with most chemicals, ensuring that it maintains its integrity over time even in harsh conditions. also, this tape is effective at preventing chemical leakage during storage and transport, thereby enhancing safety measures in various applications. The ability to maintain performance in extreme environments reduces the need for frequent replacements, ultimately lowering operational costs. Industries such as manufacturing and food processing benefit significantly from this characteristic, as the risk of contamination is minimized while ensuring productivity remains unaffected. The reliability of PTFE raw material tape under chemical exposure highlights its essential role in facilitating efficient operations across multiple sectors.
Durability of PTFE Tape in Harsh Environments
PTFE tape demonstrates exceptional durability, particularly in harsh environments where extreme temperatures and aggressive chemicals are common. Its structure allows it to withstand heat up to 370°C and cold down to -190°C without losing integrity. This thermal stability makes PTFE tape suitable for applications in industries such as aerospace, food processing, and electrical insulation. furthermore, PTFE’s resistance to various chemicals ensures that the tape remains effective even when exposed to corrosive substances that would typically degrade other materials. This resilience means that PTFE tape maintains its performance characteristics over time, providing reliable sealing solutions in demanding applications. Furthermore, its low friction surface minimizes wear and tear during operation, enhancing its longevity compared to conventional sealing materials. Overall, PTFE tape proves to be a dependable choice for manufacturers seeking durable solutions in challenging conditions.
Non-Stick Properties of PTFE Raw Material Tape
The non-stick properties of PTFE raw material tape significantly contribute to its versatility in various applications. This unique characteristic allows the tape to repel substances, preventing adhesive buildup and enabling easy removal when necessary. Industries such as food processing and pharmaceuticals benefit greatly, as the tape minimizes contamination risks and ensures compliance with hygiene standards. also, its non-stick nature enhances durability, allowing for repeated use without degradation of performance. This quality proves invaluable in assembly lines and manufacturing processes where efficiency and cleanliness are paramount. Furthermore, in high-temperature environments, PTFE tape maintains its non-stick properties, ensuring it remains effective in preventing material adhesion even under heat stress. Overall, these attributes position PTFE raw material tape as an essential component for maintaining operational efficiency across diverse industrial settings.
PTFE Tape in Electrical Insulation Applications
PTFE raw material tape plays a vital role in the field of electrical insulation due to its excellent dielectric properties. By providing a high level of resistance to electrical currents, this tape ensures safety and reliability in various electrical applications. Its low friction surface also aids in minimizing wear and tear while facilitating smoother operations within electrical components. Furthermore, the ability of PTFE tape to withstand extreme temperatures enhances its utility in environments where conventional insulation materials may fail. In addition, its resistant nature to both chemicals and moisture contributes to maintaining the integrity of electrical systems over time. Industries such as aerospace and telecommunications benefit significantly from these characteristics, as PTFE tape effectively acts as insulation for wires, cables, and connectors, ensuring optimal performance even under demanding conditions. This versatility makes it an essential choice for engineers seeking reliable solutions that boost the longevity and efficiency of electrical systems.
original Uses of PTFE Raw Material Tape in Manufacturing
PTFE raw material tape finds diverse applications in manufacturing due to its unique characteristics. In the automotive industry, it is a reliable sealing material, effectively preventing leaks in critical systems. The aerospace sector utilizes PTFE tape for its lightweight properties and ability to withstand extreme temperatures, ensuring safety and performance during flight. In the realm of electronics, this tape provides essential insulation for wiring and circuitry, enhancing reliability in high-performance devices. Furthermore, manufacturers often employ PTFE tape in the production of chemical processing equipment, where it protects against corrosive substances.
Another original application is within the food processing industry. PTFE raw material tape acts as a non-stick barrier for various machinery components, promoting efficiency and reducing maintenance costs. Its durability under high stress and exposure to harsh environments makes it a preferred choice in settings that require consistent performance. The integration of PTFE tape into these manufacturing processes not only improves operational efficiency but also contributes to the longevity of equipment by reducing friction and wear.
Conclusion
PTFE raw material tape plays an essential role in various industries due to its unique properties and versatility. Its exceptional chemical resistance, durability, and non-stick attributes make it a preferred material for sealing and insulation tasks. Industries benefit significantly from these qualities, ensuring operational efficiency even in demanding environments. For instance, in electrical insulation applications, the tape’s reliability contributes to the safety and longevity of systems that require high-performance materials. Moreover, original uses of PTFE tape span multiple sectors, including food processing and telecommunications. As industries continue to evolve, the importance of durable and efficient materials like PTFE raw material tape will become increasingly clear, driving advancements in manufacturing processes and operational standards.
FAQs
What is PTFE raw material tape used for?
PTFE raw material tape is used for sealing, insulation, and protection in various industries, including electrical, food processing, and manufacturing.
How does PTFE tape resist chemicals?
PTFE tape is chemically inert due to its unique molecular structure, allowing it to withstand exposure to a wide range of corrosive substances without degrading.
Is PTFE tape safe for food applications?
Yes, PTFE tape is safe for food applications as it maintains hygiene standards and prevents contamination due to its non-stick properties.
Can PTFE tape handle extreme temperatures?
PTFE tape can tolerate extreme temperatures ranging from -190°C to 370°C, making it suitable for use in demanding environments.
How long can PTFE raw material tape last in harsh conditions?
PTFE raw material tape has a long lifespan in harsh conditions due to its durability and resistance to chemicals, reducing the need for frequent replacements.
Does PTFE tape provide electrical insulation?
Yes, PTFE tape offers excellent electrical insulation properties and high resistance to electrical currents, making it ideal for various electrical applications.
Is there any risk of contamination with PTFE products?
PTFE products are designed to minimize contamination risks due to their non-stick surface and chemical resistance, ensuring safe use in sensitive environments.
What are the maintenance requirements for PTFE raw material tape?
this requires minimal maintenance due to its non-stick nature; regular inspections ensure that it remains effective without degradation.
Are there different grades of PTFE tape available?
Yes, various grades of PTFE tape are available in the market; these are tailored for specific applications based on their thickness and chemical resistance capabilities.