main Takeaways
PTFE raw material tape stands out for its blend of efficiency and performance across multiple sectors. Its remarkable dielectric properties ensure minimal signal loss, making it indispensable in cable insulation, especially for high-frequency applications. furthermore, PTFE’s resilience to extreme temperatures enhances durability in environments characterized by significant thermal shifts. Its non-stick and chemical-resistant features are important for the chemical industry, providing reliable protective coatings that prevent equipment corrosion and reduce maintenance demands. As industries seek solutions that marry longevity with performance, PTFE tape emerges as a cost-effective choice that ultimately minimizes operational expenses and downtime. The versatility of PTFE tape in diverse applications not only reinforces its essential role in contemporary manufacturing but also supports innovations in technology and industrial practices.
Benefits of PTFE Raw Material Tape
PTFE raw material tape offers numerous advantages that make it ideal for a range of applications. One main benefit is its outstanding dielectric properties, which significantly minimize dielectric loss, ensuring high efficiency in cable insulation. This makes PTFE cable wrapping tape particularly suitable for high-speed transmission line applications and essential in maintaining signal integrity in advanced data communication systems. also, the tape’s low friction surface reduces wear and tear on cables, enhancing their longevity. In the chemical industry, PTFE’s non-stick characteristics and resistance to harsh chemicals allow it to function effectively as a protective coating, preventing corrosion and damage to industrial containers. Its resilience to extreme temperatures further solidifies its reputation for durability across various environments. Moreover, the versatility of PTFE wrapping film extends to numerous sectors including telecommunications and aerospace, ensuring reliable performance in high-frequency circuits. Overall, the cost advantages offered by high-speed cable wrapping film solutions foster notable savings while promoting enhanced operational efficiency within multiple industries.
High efficiency in Cable Insulation
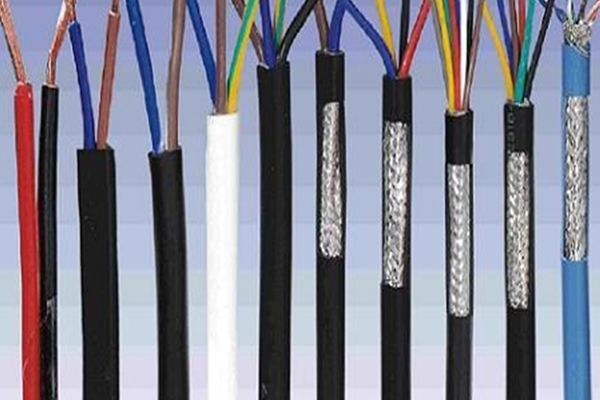
PTFE raw material tape plays a vital role in cable insulation due to its excellent dielectric properties and low dielectric loss. This tape minimizes signal interference and maintains high fidelity during data transmission, making it particularly effective for high-frequency applications such as telecommunications and data centers. The material’s stable dielectric constant contributes to reliable performance, ensuring that cables can operate efficiently over a wide temperature range. furthermore, the low friction surface of PTFE enhances the durability of cables by reducing wear during installation and usage. Its resilience against extreme environmental conditions, including moisture and chemicals, further protects the integrity of insulated cables. By utilizing PTFE raw material tape, manufacturers can achieve safer, more efficient cable designs that meet the demands of modern high-speed communication networks.
Performance in Chemical Industry Coatings
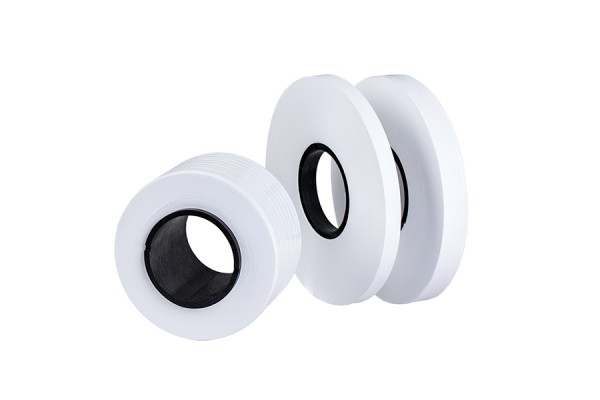
PTFE raw material tape stands out in the chemical industry for its superior coating capabilities. Its non-stick properties prevent adhesion, making it an ideal choice for lining industrial containers that handle aggressive chemicals. This feature significantly reduces maintenance needs and extends the lifespan of equipment, thereby minimizing operational downtimes. The durability of PTFE allows it to withstand harsh environments, providing reliable protection against corrosion and wear. furthermore, PTFE’s chemical resistance ensures that coatings maintain their integrity over time, even when exposed to solvents and acids. This makes it a helpful asset for various applications, from gaskets to seals in pumps and valves. The effectiveness of PTFE in these contexts not only enhances operational efficiency but also promotes safety by preventing leaks and failures, a important factor in chemical processing industries. Overall, the versatility of PTFE raw material tape solidifies its role as an essential component in providing effective protective coatings for challenging applications.
Durability and Temperature Resilience
PTFE raw material tape offers exceptional durability, maintaining its integrity under prolonged mechanical stress and environmental exposure. Its unique fibrous micropore structure contributes to strong creep resistance, preventing deformation over time. This makes it reliable for use in demanding applications, where constant performance is essential.
Temperature resilience is another main aspect of PTFE tape. It can withstand extreme conditions ranging from -150℃ to 260℃ without losing its physical or dielectric properties. This broad thermal tolerance enables the tape to function effectively in environments where temperature fluctuations are frequent or severe, such as in aerospace, high-frequency communication cables, and industrial machinery.
Moreover, PTFE’s chemical inertness supports its stability under harsh conditions, including exposure to moisture and corrosive substances. These characteristics ensure that insulation and protective coatings made from PTFE tape remain stable and effective longer than many alternative materials. This durability reduces maintenance needs and helps ensure consistent performance in critical systems.
Choosing materials with reliable durability and temperature resilience like PTFE raw material tape helps achieve sustained efficiency across various industrial challenges.
Versatile applications of PTFE Tape
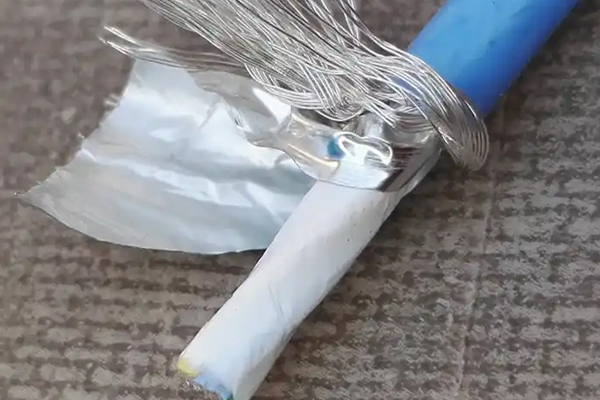
PTFE raw material tape is highly versatile, finding utility in countless applications across various industries. Its non-stick and chemical-resistant properties make it ideal for use in insulation for cables, which require reliable performance under demanding conditions. In the chemical industry, PTFE tape acts as a protective coating, safeguarding machinery and equipment from corrosive substances and wear. Its effectiveness extends to high-speed data transmission systems, where low dielectric loss is important for maintaining signal integrity. Furthermore, PTFE tape’s durability against extreme temperatures enhances its application in environments that experience drastic thermal fluctuations. This adaptability not only contributes to the longevity of components but also promotes efficiency in operations where reliability is essential. As the demand for advanced materials grows, PTFE raw material tape continues to establish itself as a go-to solution across diverse fields, underscoring its importance in modern manufacturing and technology.
PTFE Tape for High-Speed Data Transmission
PTFE raw material tape plays a vital role in high-speed data transmission applications, particularly in environments that demand minimal signal loss and exceptional reliability. Its low dielectric loss and stable dielectric constant make it an excellent choice for insulating cables used in advanced communication systems. As data rates continue to climb, especially within the realms of 6G technology and AI servers, having insulation that can handle these frequencies without deteriorating is important. The compatibility of PTFE with various high-frequency transmission requirements allows for seamless integration into existing infrastructures. Moreover, the unique properties of modified PTFE provide an edge over traditional insulating materials by maintaining performance under extreme conditions, such as temperature fluctuations and humidity. This reliability enhances overall system efficiency by reducing downtime and ensuring consistent data flow, making PTFE tape a main component for industries relying on high-speed communications.
Enhanced protection with PTFE Coating
PTFE coatings offer significant advantages in various industrial applications through their exceptional non-stick and chemical resistance properties. These characteristics make PTFE an ideal choice for lining industrial containers, protecting equipment from corrosive substances, and minimizing wear. The unique composition of PTFE ensures that surfaces remain smooth, reducing friction and facilitating easier maintenance. This durability is essential in sectors like food processing and pharmaceuticals, where hygiene and material compatibility are paramount. Furthermore, PTFE’s resilience against extreme temperatures, from -150 to 260℃, guarantees performance stability under harsh operating conditions. Its application extends to gaskets and seals used in valves and pumps, enhancing sealing capabilities while preventing leakage. Overall, the use of PTFE as a protective coating significantly contributes to operational efficiency by mitigating downtime related to corrosion and wear while maintaining equipment integrity across diverse environments.
Cost advantages of PTFE Solutions
PTFE solutions provide significant cost benefits across various industries. Their long lifespan reduces the frequency of replacements, leading to lower long term expenses for manufacturers and consumers alike. The efficiency of PTFE raw material tape in insulation applications minimizes energy loss, which translates to decreased operational costs for businesses that rely on high-performance cables. also, the resistance of PTFE to chemical reactions and extreme temperatures means less maintenance and repairs are necessary over time, further reducing costs.
Moreover, PTFE coatings can lower friction and wear on equipment, enhancing operational efficiency and allowing machinery to perform optimally for longer durations. The initial investment might be higher compared to alternative materials, but when considering durability and reduced need for replacements or repairs, PTFE solutions offer a more economical choice overall. As industries increasingly seek to optimize budgets without compromising quality or performance, the cost advantages of PTFE solutions become increasingly appealing.
Conclusion
PTFE raw material tape demonstrates considerable advantages across various applications, chiefly due to its excellent properties and usability. The unique attributes of PTFE, such as its low dielectric loss and high chemical resistance, ensure reliability in critical operations like cable insulation and protective coatings. Industries relying on high-speed data transmission benefit significantly from its ability to maintain signal integrity in the face of demanding conditions. furthermore, PTFE’s durability against extreme temperatures enhances its long term performance, contributing to reduced maintenance costs and extended equipment lifespans. This combination of efficiency, performance, and cost-effectiveness positions PTFE tape as a helpful solution across diverse sectors. Its versatility continues to inspire innovation in material applications, underscoring the necessity for advanced materials in an evolving industrial situation. Embracing PTFE raw material tape can lead to improved operational efficiency and safety, making it indispensable for future advancements in technology and manufacturing processes.
FAQs
What is PTFE raw material tape?
PTFE raw material tape is a high-performance, fluoropolymer-based tape known for its excellent dielectric properties and chemical resistance, making it suitable for insulation and protective coatings in various applications.
How does PTFE tape improve cable insulation?
PTFE tape enhances cable insulation by minimizing dielectric loss and preventing signal interference, which is essential for maintaining high fidelity in data transmission.
Can PTFE raw material tape withstand extreme temperatures?
Yes, PTFE tape can endure extreme temperatures ranging from -150℃ to 260℃ without losing its physical or dielectric properties, ensuring reliable performance in harsh environments.
What industries benefit from using PTFE coatings?
PTFE coatings are beneficial in industries such as chemical processing, food production, pharmaceuticals, and telecommunications due to their non-stick properties and resistance to corrosion.
Is the initial cost of PTFE solutions higher than alternatives?
While PTFE solutions may have a higher initial cost compared to other materials, their long lifespan and lower maintenance needs typically result in reduced overall expenses over time.